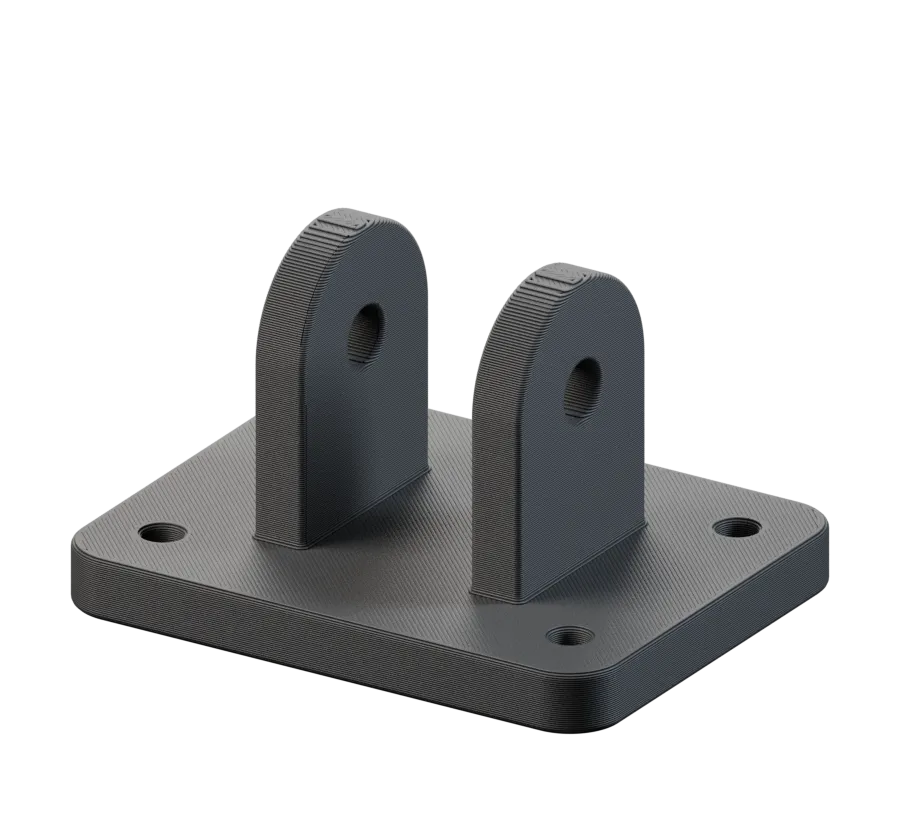
PA12-CF10 Fiberon™ material render of Linkage pivot clevis, showing the printed surface and component geometry.

PA12-CF10

Make stiff nylon brackets, fixtures and equipment parts in Polymaker Fiberon PA12-CF10. We print this carbon-fibre-reinforced FDM grade in-house and help plan the load direction, connections and final fit.

✓
10% carbon-fibre-reinforced nylon
✓
Rigid fixtures and brackets
✓
Lower moisture sensitivity than PA6
✓
Custom FDM working components
Technology

FDM

Post-processing
Tapping (internal threads)
Heat-set threaded inserts
Support removal
Colours

Polymaker

Material overview

Fiberon PA12-CF10 combines PA12 nylon with 10% carbon-fibre reinforcement for rigid functional components. It is useful for mounting parts, fixtures and guides where stiffness is important and a nylon base polymer suits the job.

Why choose PA12-CF10?

This is a reinforced FDM filament, not the Formlabs PA12 powder used in our SLS service. The manufacturer reports lower moisture sensitivity than PA6-based materials, although the filament still needs dry handling. We prepare the material and build approach around the component.

Typical applications

Equipment brackets

Position custom mounting points and supporting ribs around machinery.

Assembly fixtures

Hold and locate a component for a repeatable operation.

Guides and interfaces

Combine locating details and attachment features in a working nylon part.

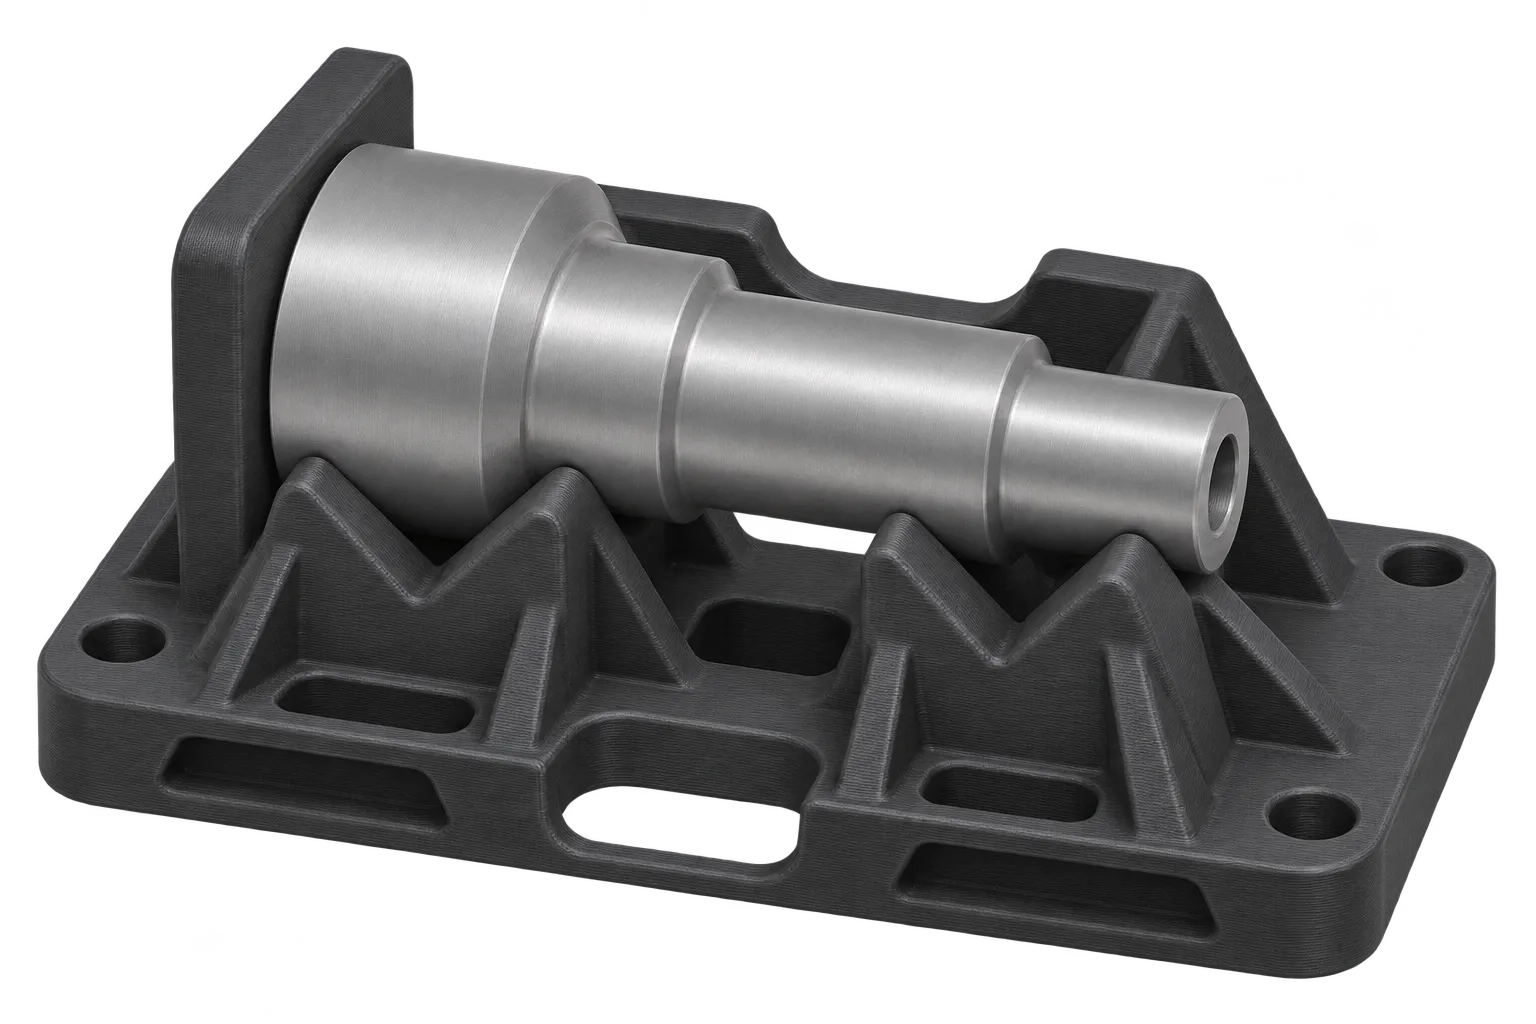
Charcoal fibre-reinforced polymer locating fixture supporting a stepped metal workpiece in shaped seats, with an end stop and open mounting holes.

Choose stiffness for the locating body.

The illustrated nest uses shaped seats and an end stop to position the workpiece. PA12-CF10 is a reinforced FDM option when the fixture should hold its shape instead of flexing around the component.

Best suited to

Rigid nylon fixtures, guides and mounting parts.

What to consider

This is not the unfilled PA12 powder used in SLS. Its print direction, support needs and surface are different.

Make the first sample useful

Mark the surfaces that locate the workpiece and the direction of force. Leave clearance for insertion and avoid using a thin printed feature as an unreviewed clamp.

Material stiffness starts with a sensible structure.

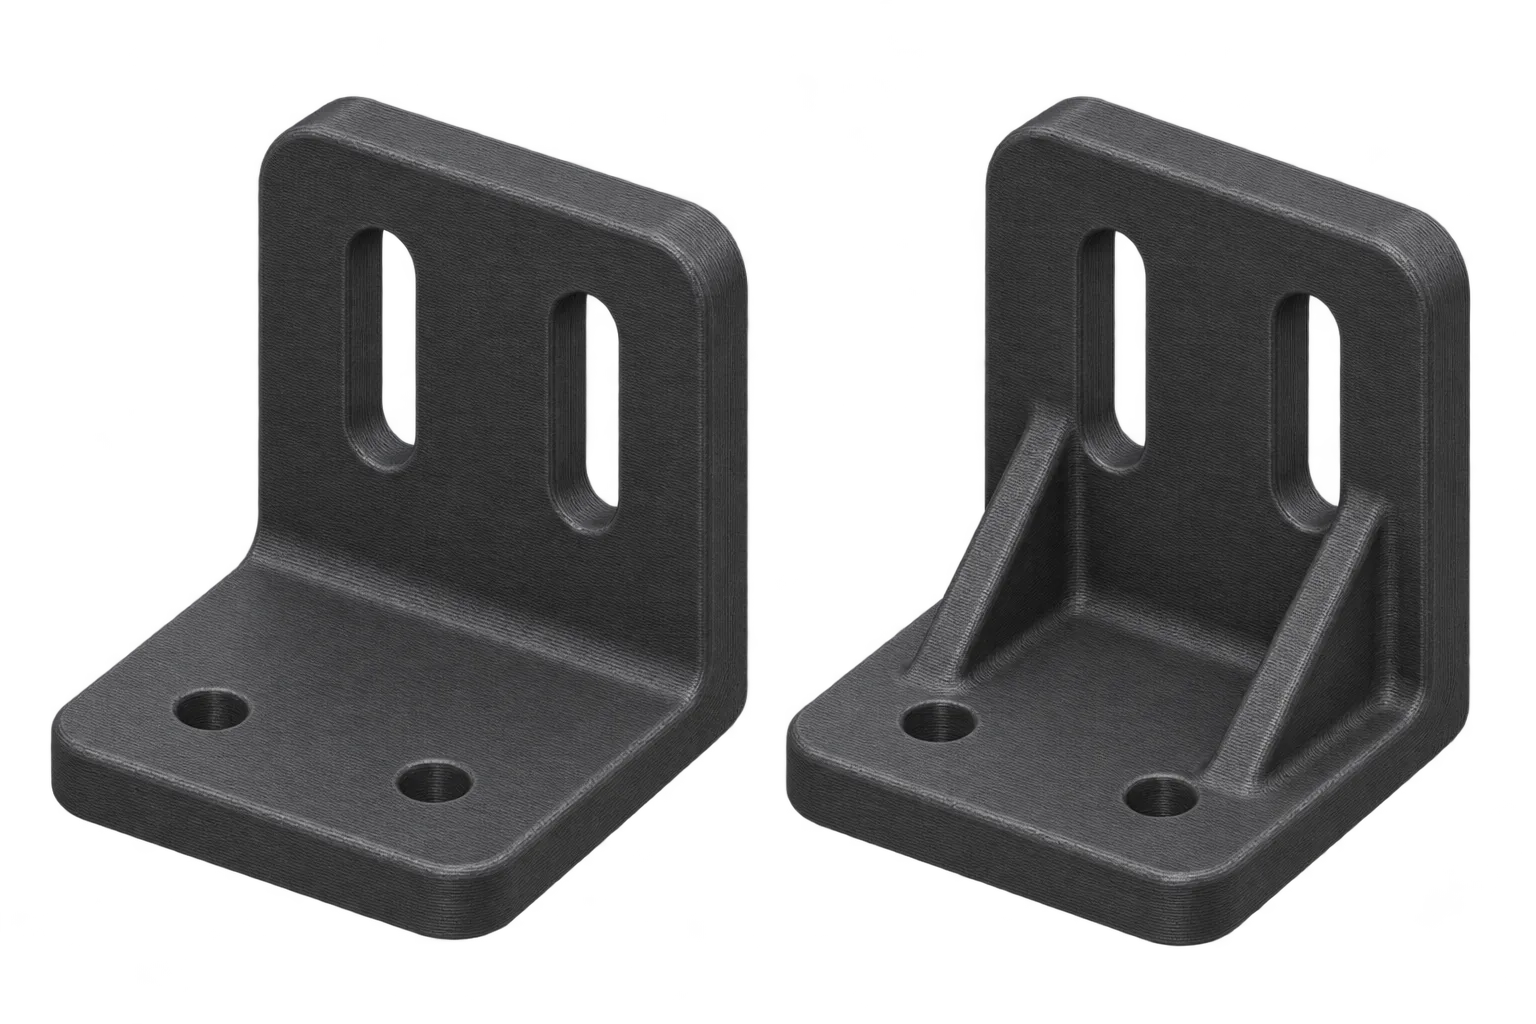
The bracket comparison shows how supporting ribs change the way a corner carries load. Fibre reinforcement helps the material resist deformation, but it does not replace a well-supported shape.

Match the build to the load

We plan print orientation around the forces at the mounting points. Strength across layers differs from strength along the printed paths.

Protect contact and fixing areas

Leave useful material around holes and spread clamping pressure where needed. A fibre-filled surface may mark a delicate workpiece; a replaceable contact pad can help.

Plan heat treatment and fit together

If annealing is part of the agreed process, we consider its effect on dimensions before final fit checks. The first fixture establishes the reference for repeat orders.

Explore the Printing Guide →

Two charcoal FDM brackets showing an unreinforced corner and the same bracket with supporting ribs and accessible mounting holes.

Order your Fiberon PA12-CF10 part.

Send the design and quantity

Send the workpiece CAD or locating dimensions with the fixture. Identify the applied forces, mounting method and surfaces where a fibre-filled finish could affect contact. No usable CAD yet? Send a drawing or photo to discuss the next step.

Compare price and plan delivery

Price depends on the size and geometry, quantity and selected finishing. Compare the available options online and tell us when you need the parts. We review custom requirements with you and confirm timing once the production brief is clear.

Agree the finish and fit

Available options include tapped internal threads, heat-set threaded inserts, where the design allows. Printed parts retain a layer pattern. We plan important fits and visible surfaces around the build, and discuss further finishing where needed. Choose from the colours shown for this material when quoting.

Start with one part or a batch. We make the components in-house using FDM and retain the agreed production details for repeat orders.

Upload CAD & get a quote →   Discuss your part →

Technical properties

Manufacturer test data helps compare grades. Printed-part performance also depends on the design and print direction. Our team can help interpret the values for your application.

Source: Fiberon PA12-CF10 manufacturer technical data. Polymaker PA12-CF10 provides grade-specific print-direction and moisture information. Dry-state results should not be treated as guarantees for every environment. The sheet’s annealing recommendation and the selected production condition are reviewed separately. Heat-deflection temperature is a test under a stated load, not a continuous service-temperature rating. We help interpret the values for your component.

Tensile strength

X–Y: 77.4 ± 1.1 MPa; Z: 52.2 ± 0.8 MPa — ISO 527 / GB/T 1040; dry

Tensile modulus

X–Y: 3311.2 ± 134.9 MPa; Z: 1806.6 ± 145.7 MPa — ISO 527 / GB/T 1040; dry

Elongation at break

X–Y: 4.2 ± 0.4%; Z: 5.0 ± 1.0% — ISO 527 / GB/T 1040; dry

Heat deflection temperature

105°C at 1.8 MPa; 131°C at 0.45 MPa — ISO 75

Density

1.06 g/cm³ at 23°C — ISO 1183 / GB/T 1033; material density

Material performance and test data

  • Flame classification: UL 94 HB at 1.5 mm.
  • Surface resistivity: >10¹² Ω (OL), ANSI ESD S11.11.
  • Moisture sensitivity: lower than PA6/66 and PA6-based materials, as stated in the TDS.

Compare PA12-CF10 with other materials.

Choose SLS PA12 for complex unfilled nylon shapes without attached supports. Compare PET-CF17 when a reinforced polyester suits the tooling brief.

Formlabs SLS PA12

For complex unfilled nylon geometry without attached supports.

PA6-CF20

Compare a different reinforced nylon and its dry/wet behaviour.

PET-CF17

For a stiff reinforced polyester tooling option.

Fiberon PA12-CF10 3D printing questions.

How is this different from Formlabs PA12?

Fiberon PA12-CF10 is carbon-reinforced filament printed by FDM. Formlabs PA12 is an unfilled SLS powder. They differ in geometry freedom, stiffness, surface and print-direction behaviour.

Does lower moisture sensitivity mean no drying is needed?

No. Polymaker still specifies dry storage and use for the filament. We handle preparation; the end-use environment also matters when close dimensions are important.

Is PA12-CF10 electrically conductive?

Carbon content is not enough to establish conductivity or ESD suitability. The linked sheet reports surface resistivity above 10¹² ohms; use grade-specific electrical data for the required application.

Upload your CAD and get a quote, or talk to our team about the application.